Skip to content

What Are the Top Manufacturing Automation Trends in 2026?

Manufacturing automation is changing from isolated machines into connected production systems. In 2026, manufacturers are weighing practical uses for artificial intelligence, collaborative robots, digital twins, and edge computing. The goal is not simply to add more technology. It is to improve quality, reduce unplanned downtime, and respond faster when orders or supply conditions shift.

Some changes are already visible on factory floors: a robot assists with repetitive assembly, sensors flag unusual vibration, and software helps teams adjust a production schedule. These tools can support better decisions, but results depend on reliable data, clear processes, and skilled people. A prediction is only useful when workers can check it and act on it. That matters. Not every plant needs the same system, and a rushed rollout can add cost without solving the original problem.

This overview explores the leading manufacturing automation trends expected to shape investment and operations in 2026. It considers how AI-enabled systems, flexible robotics, connected equipment, and digital simulation may work together, alongside growing attention to cybersecurity, energy use, and workforce training. The details will vary by sector and factory size. Treating every new tool as a guaranteed productivity boost would be a mistake. The more useful question is where automation removes a measurable bottleneck—and what people, maintenance, and safeguards are needed to keep it dependable.
What Are the Top Manufacturing Automation Trends in 2026?

Defining Manufacturing Automation and Its Role in 2026

Manufacturing automation is the coordinated use of machines, sensors, control software, and data to perform or support production tasks. It includes robotic arms, automated inspection cameras, and systems that adjust production settings when a machine begins to drift. In 2026, its role is broader than replacing repetitive manual work. It helps factories improve consistency, trace production problems, and respond to changing demand. People remain essential. They interpret results, maintain equipment, and make judgment calls that software may miss.

The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023, with 4.28 million robots operating in factories. The World Economic Forum’s Future of Jobs Report 2025 found that 58% of surveyed employers expect robotics and autonomous systems to transform their business by 2030. These figures show the scale of adoption, not a guarantee of returns. A robot can move parts precisely, yet a poorly integrated system may simply move a bottleneck elsewhere. That part is easy to underestimate.

Tips: Start with one measurable production problem, such as recurring inspection delays or inconsistent cycle times. Record a baseline, test the solution on one line, and include operators in the review. Check data quality and maintenance needs before expanding. A tidy dashboard is not proof that the process improved.

AI-Driven Robotics and Autonomous Production Systems

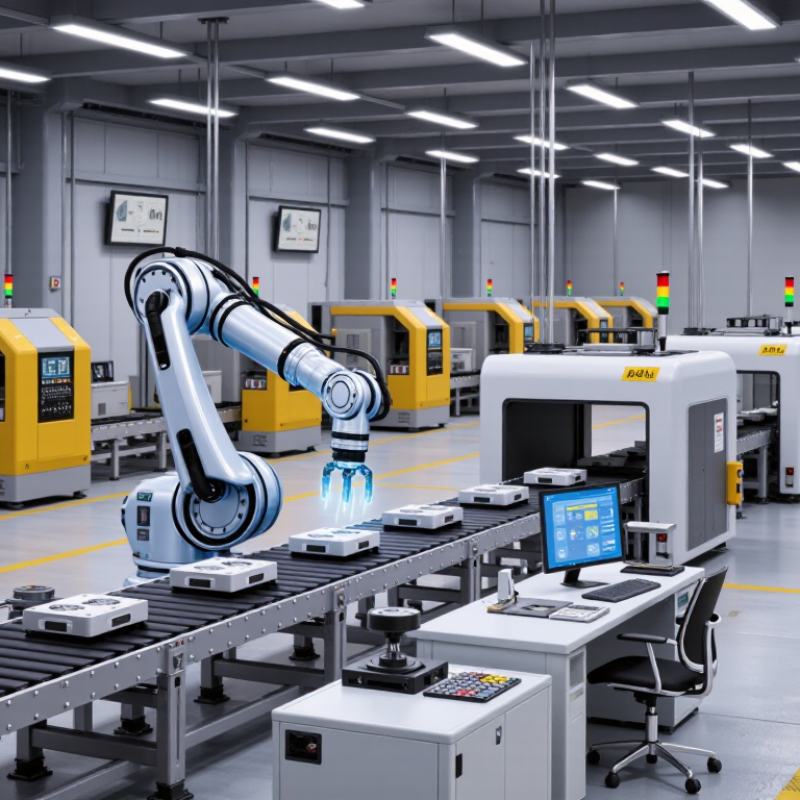
AI-driven robotics are moving beyond fixed, repetitive motions toward production systems that respond to changing conditions. A vision-guided arm can inspect a metal part, detect a misplaced hole, and adjust its grip before the next operation. Small corrections like these can reduce avoidable stoppages. They are not magic.

Autonomous production systems connect robots with sensors, scheduling software, and equipment data. When a conveyor slows, a system may reroute a task or alert an operator before work piles up. The useful detail is often practical: a warning tied to a specific machine, shift, or batch is easier to act on than a broad dashboard signal. Reliable results still depend on clean data, clear process limits, and regular testing.

People remain essential. Operators understand unusual sounds, material changes, and workarounds that sensors may miss. Automation teams should test new routines on limited production runs, record exceptions, and give staff a way to pause or override a process. Integration can be frustrating, especially when older equipment reports data inconsistently. That part is easy to underestimate. A system that works in a demonstration may behave differently beside a busy line, under dust, glare, or uneven part quality. Companies will need to judge autonomy by safe, repeatable performance—not by how little human involvement it appears to require.

Manufacturing Automation Trends in 2026: The Robotics Foundation

Global annual industrial robot installations show the scale of automation infrastructure that AI-driven robotics and autonomous production systems can build on. These are historical figures, not a 2026 forecast.

Source: International Federation of Robotics, World Robotics 2024. 2023 installations were slightly below the 2022 peak but remained above half a million units.

Connected Factories, Digital Twins, and Real-Time Data

Connected factories link machines, sensors, maintenance systems, and production schedules, giving teams a shared view of operations. A line operator might spot a motor’s rising temperature before it causes an unplanned stop. That signal matters only when it is timely, readable, and tied to a clear response.

Fast data alone is not intelligence.

Digital twins represent equipment or processes in virtual models. Engineers can compare expected cycle times with machine behavior, then test a layout change before moving physical equipment. Useful twins depend on reliable inputs and regular updates; an outdated model can create confidence without accuracy.

Keep it honest.

Teams should document sensor gaps, calibration intervals, and assumptions behind each simulation. Real-time dashboards also need restraint. Too many alerts can hide the one requiring action, especially during a busy shift. Start with a few measures, such as downtime, scrap rate, and energy use, then check whether workers can act on them. Integration often takes longer than expected, and older machines may provide inconsistent data.

That friction is real.

A shift lead may still need to verify an alert through physical inspection, especially after maintenance or sensor replacement.

Flexible Automation for Resilient and Customized Manufacturing

In 2026, manufacturers are treating flexibility as a practical response to shorter product runs, uneven demand, and supply disruptions. Instead of designing a line around one fixed product, teams are building modular workcells that can be rearranged as orders change. A robot arm, vision camera, and quick-change fixture can support several tasks, provided parts and safety checks are validated. Small batches matter.

This approach can reduce changeover delays, but only when software, tooling, and operator instructions stay aligned. Digital work instructions may guide workers through a new assembly, while sensors flag a misplaced component before it reaches packing. The useful details are often mundane: labeled connectors, reachable emergency stops, and fixtures that lock consistently. People still decide. Automation can handle repetition and awkward movements, while trained staff oversee exceptions, quality, and recovery after faults. Reconfigured systems also need documented tests and clear ownership of updates.

Resilience depends on interoperable equipment and fallback procedures when a machine or network is unavailable. A flexible cell is not automatically resilient. Extra sensors and software can add maintenance work, and smaller factories may lack specialist time to tune them. That trade-off deserves honest review: measure changeover time, defect rates, downtime, and worker workload before expanding a pilot.

Implementation Priorities, Workforce Skills, and Safety

What Are the Top Manufacturing Automation Trends in 2026? Implementation Priorities, Workforce Skills, and Safety

In 2026, successful automation starts with a production problem, not a machine purchase. Map one work cell, noting delays, awkward lifts, and recurring quality checks. Choose a small pilot with a measurable goal, such as reducing changeover time. Keep the old process available while staff test the new one. It may feel slower at first. That is useful evidence, not necessarily failure. Review downtime, defect rates, and worker feedback before expanding.

Automation also changes daily skills. Operators may need to interpret sensor alerts, adjust recipes, and recognize when a process behaves unusually. Give workers hands-on practice during normal shifts, not only a classroom overview. Safety reviews should include maintenance access, emergency stops, moving equipment, and unexpected restarts. Ask the people closest to the task where risks hide. A checklist can miss what a night-shift operator sees. Revisit safeguards after every meaningful process change.

Tips: Start with one cell. Keep instructions visible near the equipment, and name a trained person for questions on each shift. Track near misses as well as output. If operators repeatedly bypass a step, pause and investigate why; the procedure may need improvement. Don’t assume a smooth demonstration means the system is ready for full production.

What Are the Top Manufacturing Automation Trends in 2026? — Implementation Priorities, Workforce Skills, and Safety

Automation Trend 2026 Implementation Priority Evidence-Based Data Point Workforce Skills to Develop Safety and Governance Considerations Suggested Pilot KPI
Industrial robotics and flexible cells Prioritize repetitive, ergonomically demanding, or high-variation tasks where automation can be introduced without disrupting the entire production line. Start with one cell and validate changeover requirements. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023, with 4,281,585 robots operating in factories at year end. Robot operation and programming; end-of-arm tooling selection; workcell integration; troubleshooting; process-change documentation. Conduct a task-based risk assessment; guard hazardous motion; verify emergency stops and safe operating procedures; train workers before commissioning or maintenance. Compare cycle time, first-pass yield, unplanned downtime, and changeover time with the pre-pilot baseline.
AI-enabled machine vision and quality inspection Begin with a clearly defined inspection problem and a representative image dataset. Keep human review available for uncertain or safety-critical decisions. There is no single authoritative, cross-industry 2026 adoption rate for AI vision. Establish a site-specific baseline before setting an adoption target. Image and data literacy; inspection-system setup; model-output interpretation; defect taxonomy; escalation and override procedures. Test performance across product variants, lighting changes, and rare defects. Define who can accept, reject, or override automated decisions and retain traceable inspection records. Measure false acceptance and false rejection rates, inspection time per unit, and the share of results requiring human review.
Connected equipment and predictive maintenance Connect critical assets first. Use condition-monitoring data to support maintenance decisions rather than replacing established safety inspections or technician judgment. Predictive-maintenance results depend on asset type, sensor coverage, and data quality; compare performance with the facility’s own historical maintenance records. Sensor installation; basic data interpretation; asset-health monitoring; root-cause analysis; coordination between operations and maintenance. Apply lockout/tagout or equivalent energy-isolation procedures before servicing. Protect connected systems from unauthorized access and validate alarms before acting on them. Track unplanned downtime, mean time to repair, maintenance work completed as planned, and alert precision.
Digital twins and production simulation Use simulation to evaluate a specific decision, such as line balancing, layout changes, or production scheduling. Keep the model’s assumptions and data limits visible to decision-makers. Results are facility-specific. Validate model predictions against measured production data before using a twin to guide operational changes. Process modeling; production-data interpretation; model validation; scenario analysis; communication of assumptions and uncertainty. Do not use simulation alone to certify a machine or workcell as safe. Review physical changes through the facility’s normal engineering and risk-assessment process. Compare predicted and actual throughput, bottleneck time, and schedule adherence for a defined pilot period.
Collaborative robots and human-centered automation Choose tasks based on the actual interaction between people and equipment. Validate the complete application, including the robot, tool, workpiece, speed, and operating environment. Collaborative operation is application-dependent; the label “collaborative robot” does not by itself establish that a workcell is safe for shared operation. Collaborative-workcell setup; safe operating modes; task redesign; hazard recognition; operator feedback and incident reporting. Assess contact and trapping hazards, stopping behavior, tooling, and foreseeable misuse. Use applicable machinery-safety standards and verify safeguards in the installed application. Track ergonomic exposure, task completion time, near misses, and operator-reported usability.
Workforce reskilling for automation Build role-based training into the implementation plan. Involve operators and maintenance staff in design reviews, trials, and standard-work updates. The World Economic Forum’s Future of Jobs Report 2025 estimates that 39% of workers’ existing skill sets will be transformed or become outdated over the 2025–2030 period. Digital literacy; equipment troubleshooting; data-informed problem solving; human-machine coordination; continuous learning. Train workers on new hazards, safe work procedures, and stop-work authority before production launch. Confirm competency through practical demonstration, not attendance alone. Measure training completion and demonstrated competency, time to independent operation, and automation-related safety observations.
Industrial cybersecurity and secure connectivity Include security reviews when connecting operational technology, sensors, and production systems. Prioritize critical assets and maintain an inventory of connected equipment. Cyber risk varies by network architecture and exposure. Use an organization-specific asset inventory and risk assessment rather than a generic incident-rate assumption. Network and access-control basics; secure configuration; incident reporting; backup and recovery procedures; coordination between IT and operational technology teams. Restrict access by role, manage vendor and remote access, maintain tested recovery plans, and ensure security controls do not disable required safety functions. Track asset-inventory coverage, review of privileged access, backup restore-test results, and time to triage security alerts.

Sources and interpretation: Global robot figures are from the International Federation of Robotics, World Robotics 2024 (2023 data). Workforce skills figure is from the World Economic Forum, Future of Jobs Report 2025. KPI examples are recommended pilot measures, not claimed industry-wide results. Apply relevant local regulations and machinery-safety standards to each installation.

Back To Top